
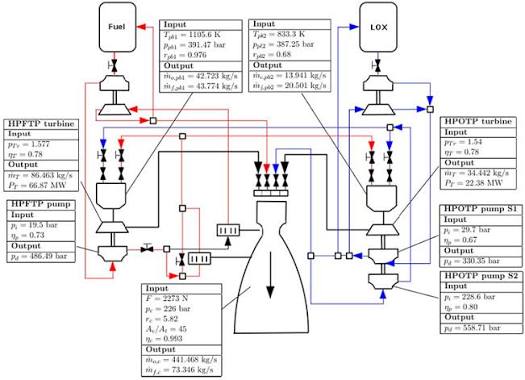
Designing liquid rocket engines is a thrilling yet unforgiving discipline where even minor miscalculations in fluid delivery can lead to catastrophic failure or inefficient combustion. If you are struggling to stabilize your engine’s performance, conducting a thorough analysis of thrust chamber plumbing across injector orifice is often the critical missing link between theoretical design and operational success. This guide breaks down complex fluid dynamics into actionable insights, helping you understand exactly how propellant behaves as it transitions from feed lines into the combustion chamber.
What Is the Role of Injector Orifices in Thrust Chamber Plumbing?
To truly master propulsion, we must first demystify the component at the heart of the system. The injector orifice is not merely a hole; it is the precise gateway that meters propellant flow, controls mixture ratios, and initiates atomization. In the context of analysis of thrust chamber plumbing across injector orifice, this component acts as the primary flow restrictor and pressure recovery device.
When analyzing this interface, engineers focus on three critical functions:
- Flow Metering: Ensuring the exact mass flow rate (m˙) matches the combustion stoichiometry.
- Atomization Control: Creating droplet sizes small enough for rapid vaporization and mixing.
- Pressure Isolation: Decoupling upstream feed system oscillations from downstream combustion instabilities.
According to fundamental principles outlined in resources like Wikipedia, the injector’s geometric design directly dictates the spray pattern and penetration depth, which are non-negotiable variables in achieving stable combustion. Without accurate plumbing analysis leading up to this point, even a perfectly machined orifice will fail to perform.
How Do You Calculate Pressure Drop Across an Injector Orifice?
The most common question in propulsion forums is, “How much pressure do I actually need?” The answer lies in calculating the pressure drop (ΔP). This metric is vital because insufficient ΔP leads to poor atomization and combustion instability, while excessive ΔP wastes pump power and adds structural weight.
Step-by-Step Calculation Guide
Follow this standardized process to determine the required differential pressure for your specific application:
- Define Target Mass Flow Rate: Determine your required m˙ based on desired thrust and specific impulse (Isp). For example, target 2.5 kg/s for a 10kN thruster.
- Select Discharge Coefficient (CdCd): Use empirical data for your orifice geometry. Sharp-edged orifices typically have a Cd of 0.60–0.65, while rounded entrances can reach 0.80–0.95.
- Measure Upstream Density (ρρ): Account for temperature and pressure. For RP-1 at 22°C, use approximately 810 kg/m³. For LOX at -183°C, use 1140 kg/m³.
- Apply the Orifice Equation: Use the standard incompressible flow formula: m˙=Cd⋅A⋅2⋅ρ⋅ΔP
- Solve for ΔPΔP: Rearrange to find ΔP=2⋅ρ⋅(Cd⋅A)2m˙2.
- Validate Against System Margin: Ensure your calculated ΔP is at least 15–20% of the chamber pressure (Pc) to prevent chugging and low-frequency instability.
Expert Insight: Always test your discharge coefficient empirically with cold flow tests using simulant fluids. Theoretical Cd values can deviate by up to 10% due to manufacturing tolerances and surface roughness in small-scale orifices.
What Factors Influence Flow Distribution Uniformity?
A perfect calculation means nothing if the flow isn’t uniform across all orifices. Non-uniform distribution creates hot spots, wall burnout, and reduced efficiency. When performing an analysis of thrust chamber plumbing across injector orifice, consider these influencing factors:
| Factor | Impact on Uniformity | Mitigation Strategy |
|---|---|---|
| Manifold Geometry | Asymmetric manifolds cause radial pressure gradients | Use annular or toroidal manifolds with symmetric inlet ports |
| Orifice Tolerance | ±0.02mm variance causes >5% flow deviation per element | Implement EDM drilling and post-manufacturing flow testing |
| Two-Phase Flow | Cavitation or gas ingestion blocks orifices intermittently | Maintain ΔP above cavitation threshold; add upstream filters |
| Thermal Expansion | Differential heating alters orifice diameter during firing | Match CTE of injector plate and manifold; use active cooling |
| Cross-Feed Coupling | Acoustic waves synchronize flow oscillations | Add acoustic dampening cavities or baffles |
Uniformity is not just about manufacturing precision; it is about designing a plumbing architecture that forgives minor imperfections through robust hydraulic balancing.
Why Does Cavitation Matter in Injector Plumbing Analysis?
Cavitation is the silent killer of injector performance. It occurs when local static pressure drops below the fluid’s vapor pressure, forming bubbles that collapse violently downstream. In the analysis of thrust chamber plumbing across injector orifice, cavitation manifests as unpredictable flow coefficients and potential erosion damage.
Identifying Cavitation Risks
- Audible Signatures: High-frequency “hissing” or erratic noise during cold flow testing.
- Flow Hysteresis: Mass flow rate differs between ramp-up and ramp-down at identical inlet pressures.
- Visual Inspection: Pitting or surface degradation on the orifice exit face after testing.
Preventive Design Parameters
To avoid cavitation, maintain a Net Positive Suction Head (NPSH) margin. Specifically, ensure the pressure at the vena contracta remains above vapor pressure. A practical rule of thumb is to keep the inlet-to-vapor-pressure ratio (Pinlet/Pvapor) above 2.5 for cryogenic propellants and above 1.8 for storable propellants. Additionally, rounding the orifice inlet edge reduces the severity of the vena contracta, raising the cavitation inception number significantly.
How Do Manufacturing Tolerances Affect Performance Predictions?
In academic models, orifices are perfect circles. In reality, they are not. Understanding tolerance stack-up is essential for realistic analysis of thrust chamber plumbing across injector orifice.
Consider a nominal 0.5mm orifice with a ±0.025mm tolerance. The area varies from 0.177 mm² to 0.221 mm²—a 25% swing in flow area. Since mass flow is directly proportional to area, your actual mixture ratio could shift dramatically from element to element.
Best Practices for Tolerance Management:
- Specify Area, Not Diameter: Call out minimum/maximum flow area rather than linear dimensions to account for out-of-roundness.
- Batch Sorting: Measure every orifice post-fabrication and group them by actual flow rate to balance the injector face.
- Statistical Modeling: Run Monte Carlo simulations using measured tolerance distributions to predict worst-case mixture ratio excursions before hardware fabrication.
- Surface Finish Specs: Specify Ra < 0.4 µm for orifice bores to reduce boundary layer effects and improve Cd predictability.
Ignoring tolerances turns your carefully engineered analysis of thrust chamber plumbing across injector orifice into an expensive guessing game.
FAQ: Common Questions About Injector Orifice Analysis
Q1: What is the recommended pressure drop ratio for stable combustion?
For most liquid rocket engines, a pressure drop across the injector equal to 15–25% of chamber pressure is recommended. This provides sufficient damping against combustion instability while avoiding excessive pump requirements. Engines operating below 10% ΔP/Pc are highly susceptible to chugging and require additional stabilization devices.
Q2: Can I use water for cold flow testing instead of actual propellants?
Yes, water is excellent for hydraulic characterization and verifying flow distribution. However, you must apply density and viscosity corrections when scaling results to actual propellants. Water cannot replicate cavitation behavior or two-phase flow characteristics of cryogens, so plan for simulant testing with appropriate fluids for those phenomena.
Q3: How does orifice length-to-diameter (L/D) ratio affect discharge coefficient?
Short orifices (L/D < 1) behave as sharp-edged apertures with lower Cd (~0.62) and higher sensitivity to inlet conditions. Long orifices (L/D > 4) develop internal boundary layers, increasing Cd toward 0.80+ but becoming more sensitive to viscous effects and surface roughness. Most rocket injectors operate in the L/D = 2–4 range as a compromise between flow stability and manufacturability.
Q4: What software tools are best for modeling injector plumbing?
Industry-standard tools include ANSYS Fluent and Siemens STAR-CCM+ for CFD analysis of internal flows and spray formation. For system-level plumbing analysis, ESI SimulationX or custom MATLAB/Simulink models provide faster iteration cycles. Always validate computational results against analytical benchmarks and cold flow test data.
Q5: How often should injector orifices be inspected during development?
Inspect orifices after every hot fire test and periodically during extended cold flow campaigns. Use optical microscopy or CT scanning to detect erosion, coking, or debris accumulation. Early-stage development may require inspection after every 3–5 tests until baseline performance repeatability is established.
Conclusion
Conducting a rigorous analysis of thrust chamber plumbing across injector orifice is foundational to building reliable, high-performance liquid rocket engines. From calculating precise pressure drops and managing manufacturing tolerances to preventing cavitation and ensuring flow uniformity, each parameter interconnects to define your engine’s ultimate success. Remember that theoretical models are starting points—empirical validation through systematic testing is what transforms equations into flight-worthy hardware.
Found this guide helpful? Share it with your fellow propulsion engineers on LinkedIn, Twitter/X, or your favorite aerospace forum. Let’s build better engines together! 🚀
Leave a Reply