
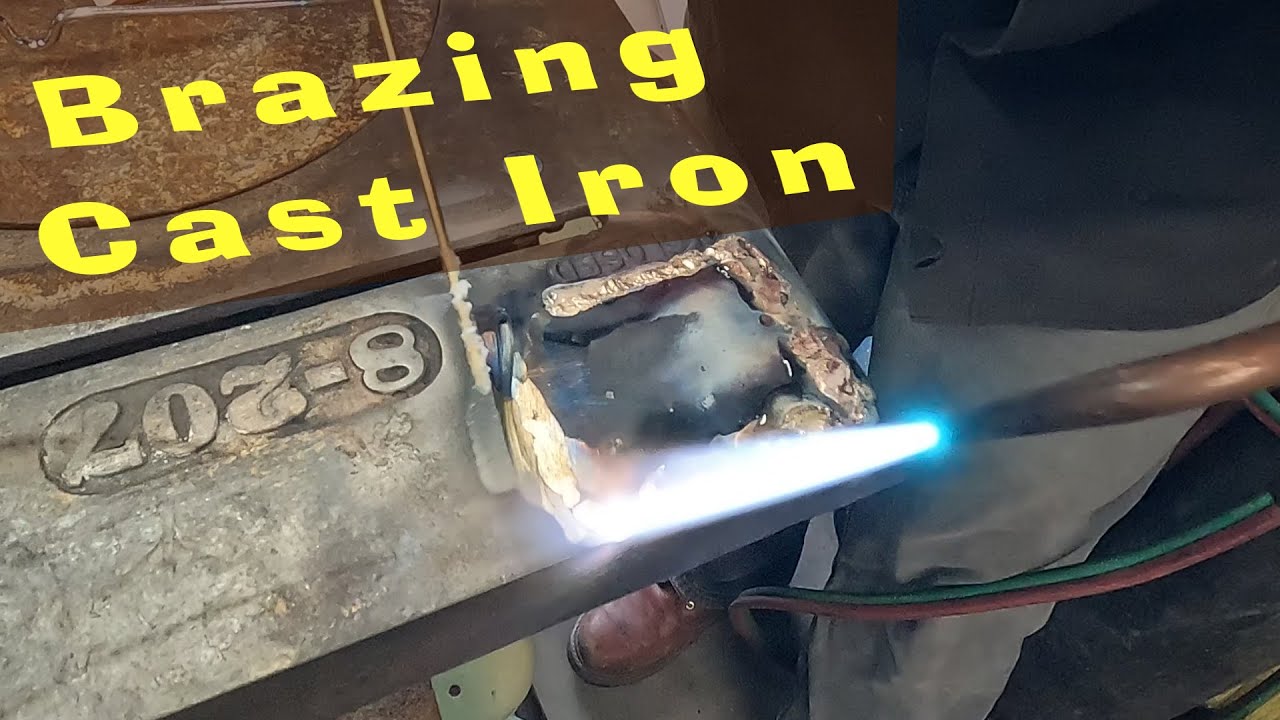
Have you ever stared at a cracked engine block or a broken vintage radiator, wondering if it’s trash or fixable? It is a frustrating situation, especially when replacement parts are expensive or obsolete. Many DIY enthusiasts and professional plumbers ask the same critical question: Can You Braze Cast Iron Acetylene Plumbing Torch? The short answer is yes, but it requires specific techniques, the right filler metal, and a deep understanding of how cast iron behaves under heat.
In this comprehensive guide, we will walk you through the science, safety, and step-by-step process of brazing cast iron using an oxy-acetylene setup. Whether you are a seasoned welder or a curious homeowner, this article will provide the clarity you need to tackle your project with confidence.
Understanding the Challenge: Why Cast Iron is Tricky
Before we light the torch, we must understand the material. Cast iron is not like steel. It has a high carbon content (usually over 2%), which makes it hard but brittle. This brittleness is the primary enemy when applying heat.
When you heat cast iron unevenly, it expands. If one part of the metal expands faster than another, internal stresses build up. Because cast iron lacks ductility, it cannot stretch to accommodate this stress. Instead, it cracks. This is why simply melting a rod onto a cold crack often leads to failure shortly after the repair cools.
The Difference Between Welding and Brazing
It is crucial to distinguish between welding and brazing, as the terms are often used interchangeably by beginners.
- Welding involves melting the base metal (the cast iron) to fuse it with the filler. This requires extremely high temperatures and creates a large “heat-affected zone,” increasing the risk of cracking.
- Brazing uses a filler metal with a lower melting point than the base metal. The cast iron itself does not melt; instead, the filler flows into the joint via capillary action.
For cast iron repairs, brazing is often superior for non-structural fixes because it introduces less heat stress to the surrounding material. However, for high-stress applications, specialized nickel-based welding rods are preferred. For the purpose of this guide, we focus on brazing, which is accessible with standard plumbing torches.
Is an Acetylene Plumbing Torch Suitable?
The core question remains: Can You Braze Cast Iron Acetylene Plumbing Torch? Yes, an oxy-acetylene torch is actually one of the best tools for this job, provided it is adjusted correctly.
Unlike air-propane torches commonly used for copper plumbing, an oxy-acetylene torch produces a much hotter flame (up to 3,500°C or 6,332°F). This concentrated heat allows for precise control. You can direct the flame exactly where needed without heating the entire piece of iron, which minimizes distortion.
However, a standard “plumbing” setup might need adjustment. Ensure your torch tips are clean and that you have the correct regulator settings. A small tip is usually better for detailed work on cracks, while a larger tip is needed for heating large masses of iron to prevent thermal shock.
Essential Tools and Materials
To achieve a professional result, you cannot rely on guesswork. Gather these items before starting:
- Oxy-Acetylene Torch Kit: With regulators and hoses in good condition.
- Bronze Brazing Rods: Specifically designed for cast iron. Look for rods with a flux coating or use separate borax-based flux. Silicon bronze is a common choice.
- Wire Brush: Stainless steel bristles are best for cleaning cast iron.
- Angle Grinder: With a grinding wheel or flap disc for preparation.
- Clamps or Vise: To hold the pieces securely.
- Safety Gear: Welding goggles (shade 5), leather gloves, and a fire-resistant apron.
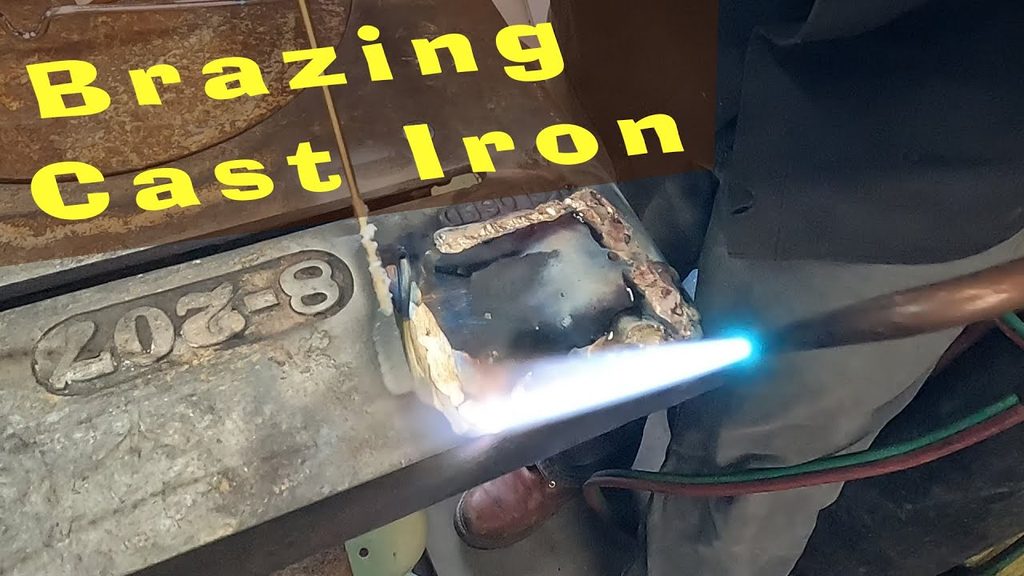
Step-by-Step Guide to Brazing Cast Iron
Follow these steps meticulously. Rushing this process is the number one cause of failed repairs.
Step 1: Preparation is Key
You cannot braze over rust, oil, or paint. The surface must be pristine.
- Use the angle grinder to bevel the edges of the crack. Create a “V” groove that is about 1/8 inch deep. This gives the brazing rod room to flow and create a strong mechanical bond.
- Clean the area thoroughly with the wire brush. Remove all debris until you see shiny, bare metal.
- Degrease the area with acetone or a dedicated metal cleaner. Any oil residue will cause porosity in the braze joint.
Step 2: Preheating the Metal
This is the most critical step that amateurs skip. You must preheat the cast iron.
- Light your oxy-acetylene torch and adjust it to a neutral flame (equal parts oxygen and acetylene).
- Slowly heat the area around the crack. Do not focus the flame directly on the crack yet. Heat a wide area, roughly 6–8 inches around the repair site.
- Aim for a temperature of approximately 500°F to 700°F (260°C to 370°C). You can test this by touching a brass brazing rod to the metal; if it melts slightly upon contact, the temperature is close. Alternatively, use an infrared thermometer for precision.
Preheating reduces the temperature gradient between the hot spot and the cold metal, preventing thermal shock cracks.
Step 3: Applying Flux and Filler
- Dip the end of your bronze brazing rod into the flux (if not pre-fluxed).
- Direct the flame at the base metal, not the rod. The goal is to heat the iron until it is hot enough to melt the rod.
- Touch the rod to the joint. If the iron is hot enough, the rod will melt and flow into the V-groove.
- Use the flame to guide the molten bronze along the crack. Allow capillary action to pull the filler deep into the joint.
Pro Tip: Keep the flame moving. Holding it in one spot for too long can burn the flux or overheat the iron, causing it to become brittle.
Step 4: Controlled Cooling
Do not quench the metal in water! Rapid cooling will guarantee a crack.
- Turn off the torch and let the piece cool slowly in still air.
- For extra safety, bury the hot cast iron in dry sand or cover it with a welding blanket. This insulates the metal and slows down the cooling process, allowing the molecular structure to stabilize.
Pros and Cons of Brazing Cast Iron
To help you decide if this method is right for your specific project, consider this comparison:
| Feature | Brazing with Acetylene | Welding with Nickel Rods |
|---|---|---|
| Heat Input | Lower, localized heat | High, widespread heat |
| Risk of Cracking | Moderate (if preheated) | High (requires skilled technique) |
| Strength | Good for non-structural loads | Excellent for structural integrity |
| Skill Level | Intermediate | Advanced |
| Cost | Low (standard rods) | Higher (specialized electrodes) |
Safety First: Handling Acetylene
Acetylene is a powerful fuel, but it demands respect. According to safety guidelines from Wikipedia’s entry on Oxy-fuel welding and cutting, improper handling can lead to flashbacks or explosions.
- Check for Leaks: Always use soapy water to check connections before lighting.
- Flashback Arrestors: Ensure your torch is equipped with flashback arrestors on both the oxygen and acetylene lines.
- Ventilation: Work in a well-ventilated area. Brazing fluxes can produce fumes that are harmful if inhaled in confined spaces.
Frequently Asked Questions (FAQ)
1. Can I use a propane torch instead of acetylene?
While possible for very small, thin pieces, a propane torch generally does not get hot enough to properly braze thick cast iron. The heat input is too low, leading to poor fusion and weak joints. An oxy-acetylene torch is highly recommended for reliable results.
2. What type of brazing rod is best for cast iron?
Silicon bronze rods are the industry standard for brazing cast iron. They offer good color matching and strong adhesion. Some professionals also use low-fuming bronze rods to reduce zinc vapor exposure.
3. Do I need to remove all the old paint?
Yes. Paint contains oils and chemicals that will contaminate the weld pool. You must grind down to bare, shiny metal for the brazing filler to bond correctly.
4. How strong is a brazed cast iron repair?
A properly executed braze is strong enough for many applications, such as sealing leaks in radiators or fixing non-load-bearing brackets. However, it is not as strong as the original cast iron. For high-stress structural components (like engine mounts), welding with nickel rods or replacing the part is safer.
5. Why did my repair crack after cooling?
This is usually due to insufficient preheating or cooling too quickly. Cast iron is sensitive to thermal shock. Always preheat the surrounding area and allow the part to cool slowly in sand or air.
6. Can I braze cast iron to steel?
Yes, brazing is an excellent method for joining dissimilar metals like cast iron and steel. Since neither metal melts completely, you avoid the formation of brittle intermetallic compounds that often occur during welding.
Conclusion
So, can you braze cast iron with an acetylene plumbing torch? Absolutely. It is a viable, cost-effective, and durable solution for many repair scenarios. By respecting the material’s brittleness, preheating adequately, and using the correct silicon bronze filler, you can restore functionality to broken cast iron items.
Remember, patience is your best tool. Rushing the heating or cooling phases is the quickest way to failure. Take your time, prioritize safety, and enjoy the satisfaction of bringing a broken piece back to life.
If you found this guide helpful, please share it with your fellow DIY enthusiasts on social media. Have you tried brazing cast iron before? Share your experiences or questions in the comments below!
Leave a Reply