
Have you ever found yourself in the middle of a critical repair job, only to realize you’re missing the specific flux required for silver brazing? It’s a frustrating scenario that many DIY enthusiasts and even some junior technicians face when trying to improvise with materials on hand. You might be staring at a tube of standard plumbing paste and asking yourself: Can plumbing flux be used for silver brazing?
The short answer is no, and attempting to do so can lead to weak joints, leaks, and potential system failures. While both products share the word “flux” and serve the general purpose of cleaning metal surfaces, their chemical compositions and intended temperature ranges are vastly different. In this guide, we will break down exactly why these two products are not interchangeable, the science behind high-temperature brazing, and what you should use instead to ensure a professional, leak-proof result.
Understanding the Difference: Plumbing Soldering vs. Silver Brazing
To understand why you cannot swap these fluxes, we first need to distinguish between the processes they support. Many people use the terms “soldering” and “brazing” interchangeably, but in the metallurgical world, they are distinct processes defined by temperature and filler metal strength.
Plumbing soldering typically involves joining copper pipes using tin-lead or lead-free solder. This process occurs at relatively low temperatures, usually between 350°F and 450°F (175°C–230°C). The flux used here is designed to activate at these lower temperatures to remove light oxidation from copper surfaces.
Silver brazing, on the other hand, is a high-temperature process. It uses filler metals containing silver, copper, and phosphorus, requiring temperatures between 1,100°F and 1,600°F (590°C–870°C). This method is common in HVAC systems, refrigeration lines, and heavy-duty industrial piping where extreme pressure and thermal stress are expected.
Why Temperature Matters
Flux is not just a cleaner; it is a chemical agent that must remain stable and active within a specific thermal window. If you use low-temperature plumbing flux in a high-temperature brazing environment, the flux will burn off almost instantly before it can protect the joint. Conversely, high-temperature brazing flux may not activate properly at the lower temperatures used for standard plumbing soldering, leading to poor wetting and weak bonds.
The Chemical Composition Breakdown
The primary reason can plumbing flux be used for silver brazing yields a negative result lies in chemistry. Let’s look at what is inside these tubes.
Standard Plumbing Flux
Most plumbing pastes are water-based or petroleum-based mixtures containing:
- Zinc Chloride or Ammonium Chloride: These are aggressive acids that clean copper quickly at low heat.
- Petroleum Jelly: Acts as a carrier to keep the flux in place.
- Wetting Agents: Help the solder flow into the capillary gap.
These ingredients are volatile. When exposed to the intense heat of an oxy-acetylene torch used for brazing, the petroleum base ignites, and the chlorides vaporize rapidly. This leaves behind corrosive residues that can eat away at the metal over time, causing pinhole leaks.
Silver Brazing Flux
Brazing fluxes are typically powder-based or paste formulations designed for extreme heat. They often contain:
- Borax (Sodium Borate): A primary ingredient that melts at high temperatures to form a glass-like shield.
- Boric Acid: Helps lower the melting point of the borax and improves fluidity.
- Fluorides: In some specialized formulations, fluorides are added to help dissolve tough oxides on stainless steel or brass.
According to technical data from industry standards, brazing fluxes are engineered to form a protective slag that prevents oxidation during the heating process. This slag must remain liquid and protective until the joint cools sufficiently. Plumbing flux simply lacks the thermal stability to perform this function. For more detailed chemical properties of borax and its industrial applications, you can refer to Wikipedia’s entry on Borax.
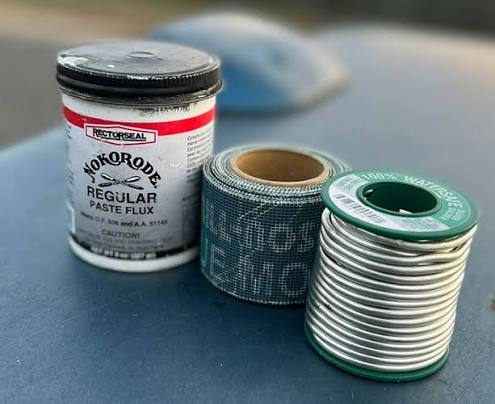
Risks of Using Plumbing Flux for Brazing
If you decide to ignore the warnings and use plumbing paste for your silver brazing project, here is what you can expect:
- Immediate Burn-Off: The flux will smoke heavily and disappear before the base metal reaches the necessary brazing temperature. Without flux protection, the copper or steel will oxidize rapidly, creating a scale that prevents the silver filler from bonding.
- Poor Capillary Action: Silver brazing relies on capillary action to draw the filler metal into the joint. Oxidized surfaces repel the filler metal, leading to voids and incomplete penetration.
- Corrosion and Leaks: The residual chlorides from plumbing flux are highly corrosive. Even if the joint appears to hold initially, the leftover chemicals can cause internal corrosion, leading to catastrophic failure months or years later.
- Safety Hazards: Burning petroleum-based flux produces toxic fumes. In confined spaces, such as under a sink or in an attic, this poses a significant health risk to the technician.
Comparison Table: Plumbing Flux vs. Brazing Flux
| Feature | Plumbing Flux | Silver Brazing Flux |
|---|---|---|
| Primary Use | Soft Soldering (Copper to Copper) | Hard Brazing (Copper, Steel, Brass) |
| Operating Temp | 350°F – 450°F (175°C – 230°C) | 1,100°F – 1,600°F (590°C – 870°C) |
| Base Ingredient | Zinc/Ammonium Chlorides | Borax, Boric Acid, Fluorides |
| Form | Paste/Gel | Powder or High-Temp Paste |
| Residue | Water-soluble, corrosive if left | Glass-like slag, must be chipped/washed |
| Oxidation Protection | Low temperature only | High temperature stability |
How to Properly Prepare for Silver Brazing
Since we’ve established that plumbing flux is not an option, let’s walk through the correct steps to ensure a successful silver braze. Following these steps will guarantee a joint that is strong, leak-free, and durable.
Step 1: Clean the Surfaces
Mechanical cleaning is just as important as chemical fluxing. Use emery cloth or a wire brush to remove all dirt, oil, and oxidation from the pipe and fitting. The metal should shine like a new penny. Any grease left on the surface will contaminate the flux.
Step 2: Apply the Correct Flux
Use a dedicated silver brazing flux. If using powder flux, mix a small amount with water or alcohol to create a thin paste. Apply a thin, even layer to the male end of the pipe. Do not apply flux to the inside of the fitting, as it can block the flow of the filler metal.
Pro Tip: Less is more. Excessive flux can create bubbles and voids in the joint. A thin, transparent coat is sufficient.
Step 3: Assemble the Joint
Insert the pipe into the fitting. Ensure there is a proper clearance gap (typically 0.002 to 0.005 inches) for capillary action to work. Wipe away any excess flux that squeezes out.
Step 4: Heat Evenly
Use an oxy-acetylene or air-acetylene torch. Move the flame around the joint to heat both the pipe and the fitting evenly. Avoid directing the flame directly at the filler rod. The goal is to bring the base metal up to temperature, not to melt the filler metal with the flame.
Step 5: Apply the Filler Metal
When the metal reaches the correct temperature (usually indicated by a dull red glow), touch the silver brazing rod to the joint. If the temperature is right, the rod will melt and be drawn into the joint by capillary action. Feed the rod around the entire circumference of the joint.
Step 6: Cool and Clean
Allow the joint to cool naturally. Do not quench it with water, as this can cause cracking due to thermal shock. Once cooled, remove the glass-like slag residue using a wire brush and warm water.
Frequently Asked Questions (FAQ)
1. Can I use rosin core solder for silver brazing?
No. Rosin core solder is designed for electronics and low-temperature plumbing. It burns away instantly at brazing temperatures and provides no protection against oxidation. It will result in a failed joint.
2. What happens if I don’t use any flux for silver brazing?
Without flux, the metal will oxidize rapidly when heated. The silver filler metal will ball up on the surface rather than flowing into the joint. This results in a weak, non-leak-proof connection that will likely fail under pressure.
3. Is there a “no-clean” flux for silver brazing?
While some modern brazing alloys contain phosphorus (such as BCuP series), which acts as a self-fluxing agent on pure copper, flux is still recommended for brass, steel, or dissimilar metals. For critical HVAC applications, using external flux is always the safer, professional choice.
4. Can I mix plumbing flux with brazing powder to make it last longer?
Absolutely not. Mixing incompatible chemicals can create unpredictable reactions, release toxic gases, and compromise the integrity of the brazing process. Always use the flux specified by the filler metal manufacturer.
5. How do I store silver brazing flux?
Keep brazing flux in an airtight container in a cool, dry place. Moisture can cause clumping in powder flux, making it difficult to apply evenly. If using a paste, ensure the lid is sealed tightly to prevent drying out.
Conclusion
So, can plumbing flux be used for silver brazing? The definitive answer is no. The chemical incompatibility, temperature limitations, and risk of corrosion make it a dangerous shortcut that compromises the integrity of your work. Plumbing flux is designed for low-temperature soft soldering, while silver brazing requires specialized high-temperature fluxes based on borax and boric acid to withstand the heat and protect the metal.
By using the correct materials and following proper preparation steps, you ensure that your joints are not only leak-free but also durable enough to withstand high pressure and thermal cycling. Don’t risk a costly callback or a system failure by improvising with the wrong flux. Invest in the right tools for the job, and your craftsmanship will speak for itself.
If you found this guide helpful, please share it with your fellow technicians or DIY friends on social media. Helping others avoid common mistakes strengthens our entire community of skilled tradespeople!
Leave a Reply